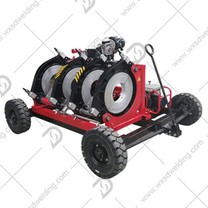
1. Preparation for welding
Welding preparation is mainly to check whether the condition of the welding machine meets the work requirements. For example, check whether the fasteners of various parts of the machine are loose or loose; check whether the electrical circuit connection of the whole machine is correct and reliable; check whether the hydraulic oil in the hydraulic tank is sufficient; confirm that the power supply matches the machine input requirements; whether the heating plate meets the requirements (Whether the coating is damaged); Trial operation of milling cutters and oil pump switches, etc.
Then put the slips of the same pipe specifications into the rack; set the heating plate temperature to the welding temperature (the welding temperature of the polyethylene pipe machine path is 200~230℃), before heating, use soft paper or cloth dipped in alcohol to wipe the heating plate The surface, but be careful not to scratch the PTFE anti-adhesive layer.
2. Welding
Welding should be operated in accordance with the parameters of the welding process card. When necessary, it should be adjusted appropriately according to changes in weather and ambient temperature. The main steps are as follows.
(1) Use a clean cloth to remove the dirt on the ends of the two pipes. Place the pipe in the frame slip so that the extension length of the two ends is equal (it should be as short as possible under the condition of meeting the requirements of milling and heating, usually 25~30mm). If necessary, the parts other than the pipe rack should be held up with a support so that the axis of the pipe is at the same height as the center line of the rack, and then fastened with slips.
(2) Insert the milling cutter, first turn on the power switch of the milling cutter, then slowly close the welding ends of the two pipes, and apply appropriate pressure until continuous chips appear at both ends. Remove the pressure, wait a moment, and then exit the activity Rack, turn off the power of the milling cutter. The chip thickness should be 0.5~1.0mm, and the chip thickness can be adjusted by adjusting the height of the milling blade.
(3) Take out the milling cutter, close the two pipe ends, and check the alignment of the two ends. The amount of misalignment at both ends of the pipe should not exceed 10% of the pipe wall thickness or 1mm, whichever is greater. It can be corrected to a certain extent by adjusting the straightness of the pipe and the elastic slip; there is no obvious gap between the two ends of the pipe when closing. The maximum width cannot exceed: 0.3mm (DN< 225mm), 0.5mm (225mm<DN<400mm) or 1.0mm (DN>400mm). If the above requirements are not met, milling should be performed again until the above requirements are met.
(4) Measure the drag force (friction resistance of the moving fixture). This pressure should be superimposed on the process parameter pressure to obtain the actual pressure. And check whether the temperature of the heating plate reaches the set value.
(5) After the temperature of the heating plate reaches the set value, put it into the rack and apply the specified pressure until the minimum curling edge on both sides reaches the specified width and the pressure is reduced to the specified value (so that the end of the tube and the heating plate just keep contact) , Endothermic.
(6) After the time is up, retreat the movable rack, quickly take out the heating plate, and then close the two pipe ends. The switching time should be as short as possible and not exceed the specified value. After cooling to the specified time, release the pressure, loosen the slips, and take out the connected pipe.